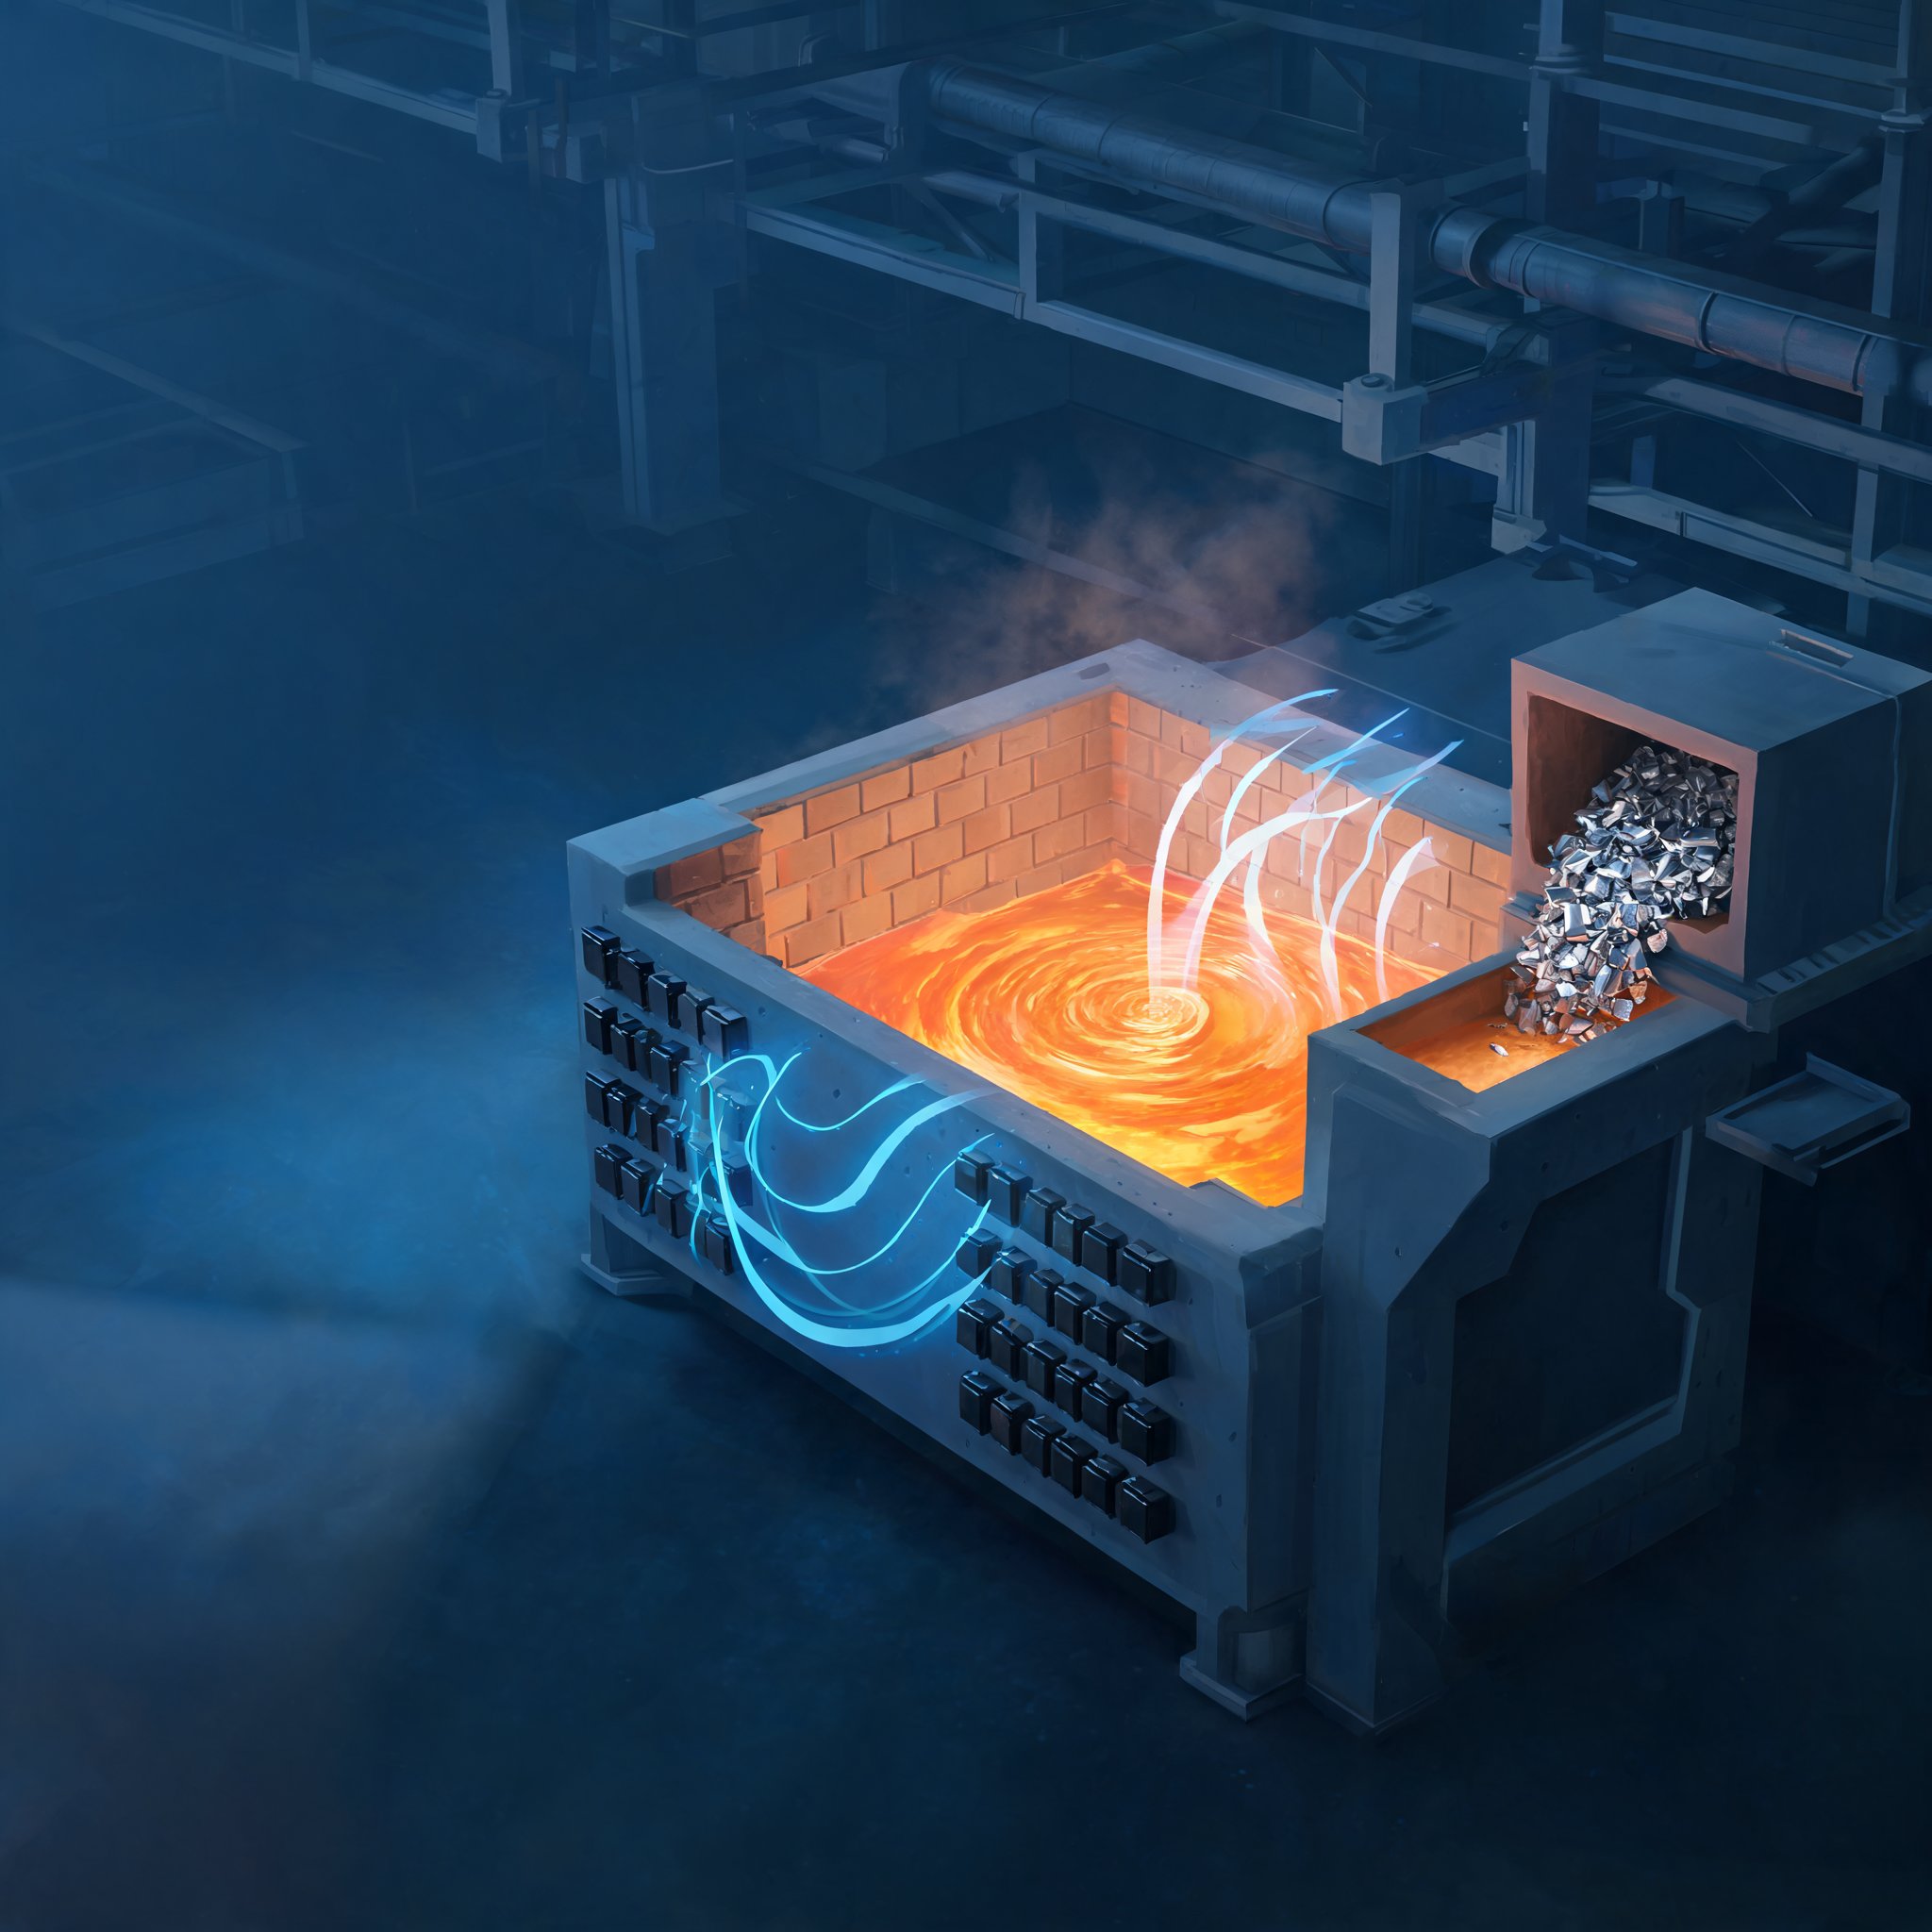
Aluminium casthouses adding post-consumer scrap face a trade-off between recycled content and melt quality, recovery and throughput. Zmag America is positioning a family of permanent-magnet devices — MagStir, MagPump and Typhoon — as a way to stir, circulate and submerge molten metal without immersing rotating parts in the bath.
Lightweight scrap, machining chips and other low-density material are difficult to charge into conventional melting furnaces, which makes efficient feeding and submergence central to recycling performance. The problem does not stop at scrap preparation: temperature and chemical composition have to stay consistent across the molten bath to meet specification, so circulation and stirring equipment must support heat transfer and metal movement while limiting process interruptions and metal loss. Conventional mechanical pumps rely on immersed rotating components that can deteriorate through contact with molten aluminium, dross accumulation and refractory debris.
From eddy-current separation to molten metal
Zmag's roots are in magnetic engineering and the commercialisation of eddy-current separation, used to recover non-ferrous metals from mixed streams; the company later moved into molten-metal applications. Its patented zPMC permanent magnetic circuit underpins equipment that stirs, circulates and submerges aluminium. Rather than a conventional electromagnetic stirring arrangement, the system uses a permanent magnetic circuit to generate the field that moves the metal, producing what the company calls a virtual impeller and avoiding immersed mechanical impellers.
Eishin Takahashi, president of Zmag America, said in an August 2025 interview that limited familiarity with the approach has held back wider adoption in the United States, observing that producers around the world tend to be conservative and prefer equipment and processes they already know.
MagStir for furnace homogenisation
MagStir is a non-contact stirring system for melting and holding furnaces that uses the permanent magnetic circuit to move the bath and even out temperature and alloy composition. Configurations cover furnaces from 15 to 200 metric tons. Because there is no immersed stirring component, casthouses can add circulation without introducing further moving parts into the melt. New Zealand Aluminium Smelters installed the system in a casting furnace and later extended it to other furnaces; a technical case study published in 2017 reported better temperature control during furnace preparation. A MagStir unit was also fitted to a casthouse furnace at Rio Tinto's Boyne Smelters in Queensland, Australia, in 2019.
MagPump and the TST trial
MagPump extends the same approach to pumping and circulating metal. It fits a standard pump well without furnace modification, has no physical impeller and is marketed as a nearly hands-free option with no consumable parts and minimal downtime. At the TANDEM Division of US secondary producer TST Inc. in Fontana, California, a seven-week trial replaced an existing mechanical pump in a production furnace. The reported findings describe smooth operation and less disturbance of the molten-metal surface, and plant management said the system avoided the splashing seen with conventional pumping as the metal level fell during draining. The technology was presented at the TMS 2023 Annual Meeting and Exhibition, where side-well, multi-chamber furnaces were discussed alongside possible additional duties such as gas injection and scrap submergence.
Typhoon submerges light scrap and chips
Typhoon addresses scrap submergence and chip melting by drawing lightweight scrap and machining chips beneath the metal surface rather than letting them sit on top. Its magnetic circuit creates a vortex-like movement that pulls material into the melt, supporting heat exchange and recovery. At Neuman Aluminium's Marktl plant in Austria, the system was added during a furnace modernisation intended to widen the range of low-density post-consumer scrap the plant can handle, including fractions with a bulk density of about 375 kg/m³. Neuman set a target of one metric ton per hour while the furnace continued to melt solid charge; in operation the system processed almost twice the planned quantity within the expected time, with low operator involvement and, according to the company, no adverse effect on melt or finished-product quality. Typhoon runs at 5–15 kW including its air-cooling blower and can submerge up to five metric tons per hour of machining chips, with vortex intensity adjustable so movement can be maintained when no scrap is being charged.
A crowded field with different approaches
Several established suppliers compete in furnace stirring, circulation and scrap submergence, though not all offer direct equivalents. ABB's AL-EMS electromagnetic stirring system has more than 430 installations, and in April 2026 the company announced a further order from Arconic for a fifth stirrer at its Hungarian casthouse. Presezzi Extrusion Group's Melting Technology division offers the L.E.C. stirrer for melting and holding furnaces. Pyrotek supplies electromagnetic pump systems and its LOTUSS low-turbulence scrap submergence technology, and its UK operations include EMP Technologies Ltd. Rockwell Automation sits in adjacent industrial automation, supplying furnace and ladle-shop control systems, as in its modernisation work for Mozal Aluminium's casthouse.
For producers taking on harder recycled feedstock, managing molten-metal movement without immersed mechanical parts may become more relevant, though the reported results remain tied to the installations described.